Diameters up to Ø450 mm
We can manufacture disc electrodes up to Ø450 mm in diameter. Component dimensions and mounting requirements are agreed based on documentation or a sample.
PRODUCTS / DISC ELECTRODES
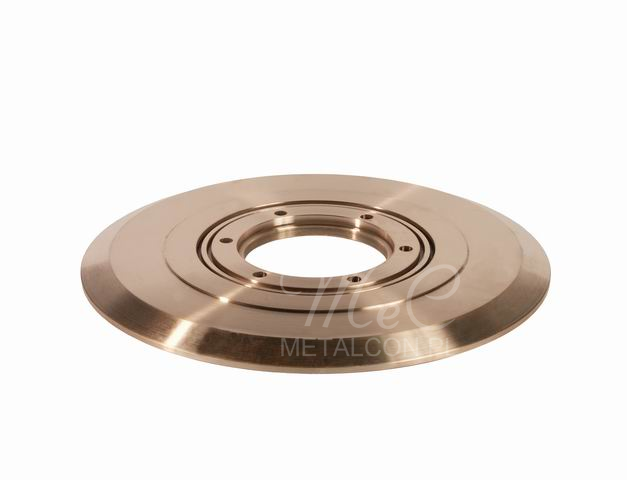
We manufacture copper alloy disc electrodes for resistance seam welding. Diameters up to Ø450 mm are available, with geometry and cooling arrangements matched to the specific application.
PROFILE / MOUNTING / COOLING
In resistance seam welding, the electrode must be matched to the equipment and operating conditions. We agree the geometry, material and cooling arrangement based on the requirements of the specific assembly.
We can manufacture disc electrodes up to Ø450 mm in diameter. Component dimensions and mounting requirements are agreed based on documentation or a sample.
The outer diameter, thickness, working profile, central bore and mounting are determined by the welding machine design and process requirements.
We manufacture electrodes with different cooling arrangements. The required configuration is selected for the specific geometry and operating conditions.
Documentation or a supplied sample defines the scope of manufacture. Before production, we agree the material, geometry and quantity.
IN-HOUSE PRODUCTION / FROM MATERIAL TO DISC ELECTRODE
We manufacture wheel electrodes using hot and cold forming. Combined with heat treatment selected to suit both the manufacturing process and the electrode material, this increases their service life compared with similar products manufactured solely by hot forging. We can manufacture these electrodes up to a diameter of Ø450 mm.
PRODUCTION / 01
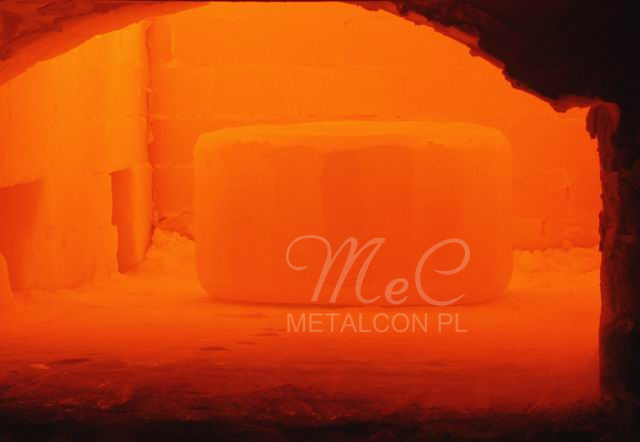
Preparation for forming begins with the material. The photo shows a semi-finished blank in the furnace — one of the process stages before forging.
PRODUCTION / 02
The heated blank moves on to further forming. Preparation and subsequent operations are selected to suit the material and the required electrode geometry.
PRODUCTION / 03
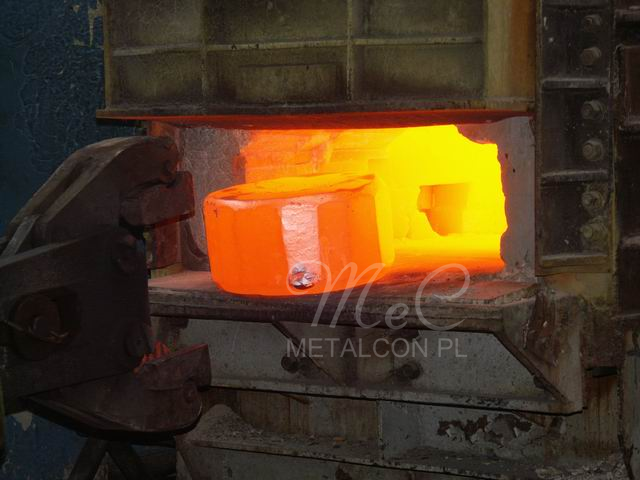
Forming shapes the material for subsequent operations. It is part of the disc electrode manufacturing process, complemented by an appropriately selected heat treatment.
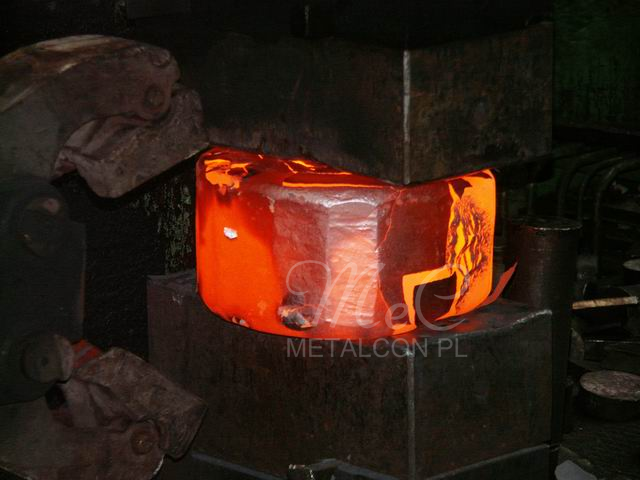
PRODUCTION / 04
Successive forming operations bring the blank closer to the required geometry. The final working profile, holes and mounting surfaces are defined by the component documentation.
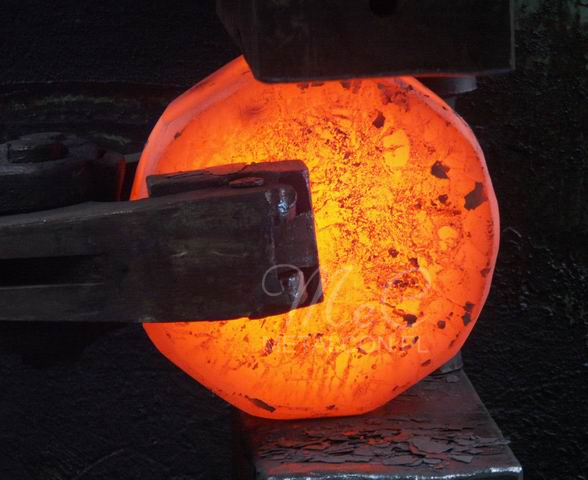
PRODUCTION / 05
Manufacturing combines hot and cold forming with heat treatment. We define the production sequence according to the alloy used and the requirements of the finished electrode.
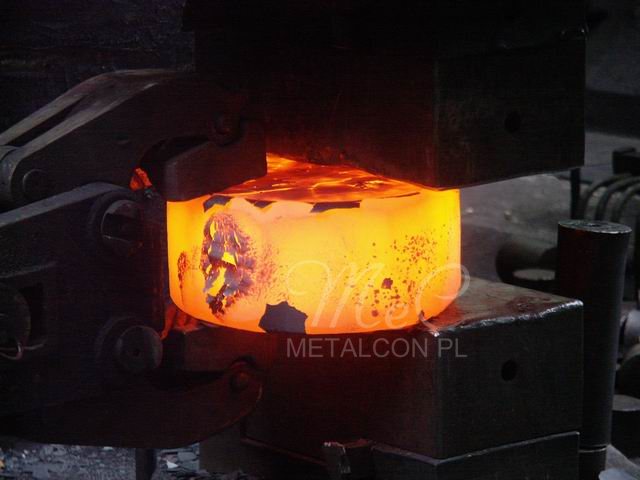
MATERIAL / PROCESS / INSPECTION
Our range includes electrodes made from class A2 and A3 copper alloys. The grade and manufacturing process are selected according to the documentation and application requirements.
Materials:
Standard wheel electrodes with a hardness of ≥75 HRB for Class A2 copper alloy (CuCrZr)
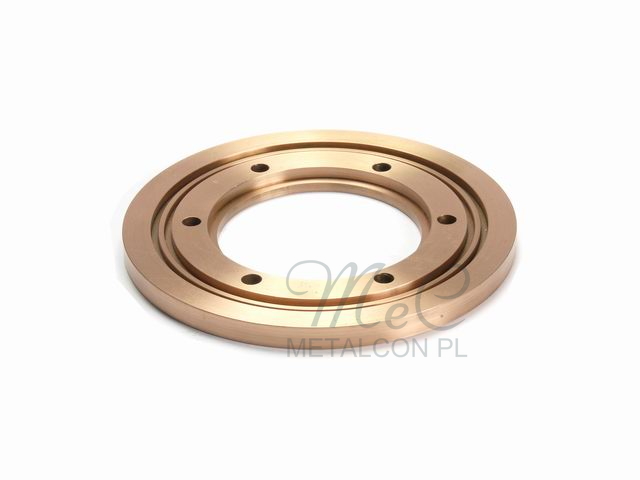
GEOMETRY / COOLING / MANUFACTURING QUALITY
The electrodes are available with a variety of cooling system configurations.
We agree dimensions, mating surfaces and inspection requirements based on the drawing. This documentation enables us to check conformity with the assembly requirements.
Dimensional and functional inspection ↗FINISHED ELECTRODES / GEOMETRY TO SPECIFICATION
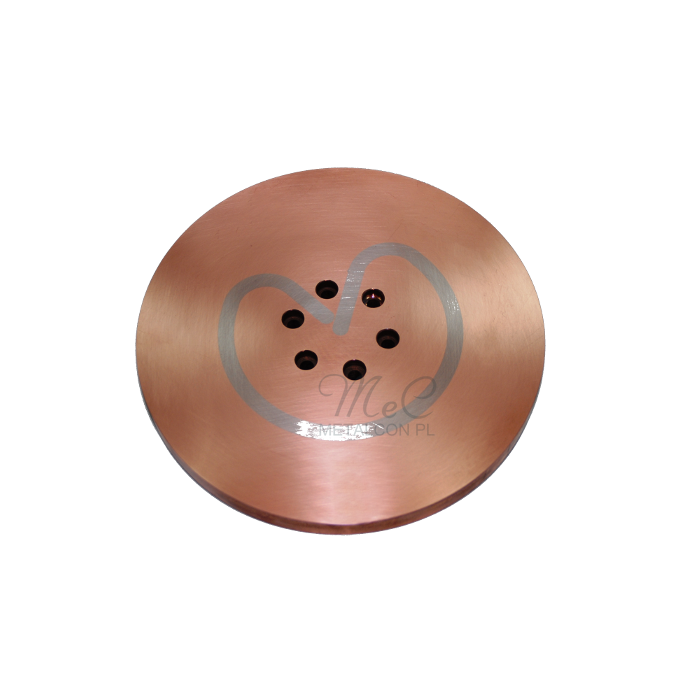
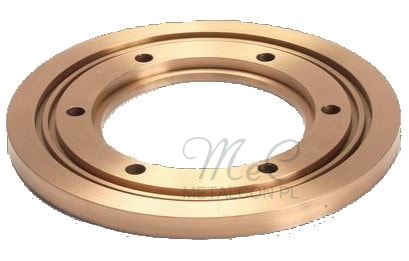
The finished disc combines the agreed geometry with a material selected for the application. We manufacture the profile, holes and mounting surfaces for the specific welding machine assembly.
Send a drawing or provide a sample. We will agree the production scope, required quantity and delivery date.
Enquire about disc electrodes ↗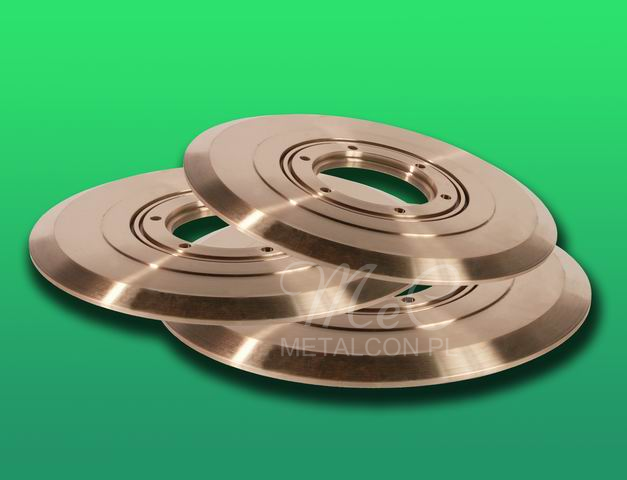
ENQUIRY / KEY INFORMATION
Send documentation showing the dimensions, working profile, holes and mounting method. You can also provide an existing disc electrode.
State the material grade and cooling arrangement. If your documentation is incomplete, describe the welding machine and the application.
Specify the required quantity and requested delivery date. For urgent requirements, we will check whether express production is possible.
PRACTICAL GUIDANCE / PREPARING AN ENQUIRY
Specify thickness, working profile, centre bore, mounting and cooling arrangement. Where relevant, attach a drawing showing channel dimensions and mating surfaces. Also provide the material grade or operating conditions, quantity and required date.
Show both sides of the electrode, its working profile and mounting. Add available dimensions and describe the machine and material being welded. Wear can change the geometry, so information from a used electrode needs assessment before a replacement is manufactured.
FROM TECHNICAL DOCUMENTATION TO FINISHED COMPONENT
A drawing, sample or description of the application is a good starting point for working together.